Case analysis of H series right-angle gearboxes in industrial wastewater treatment industry
Publication date:2025/8/29 23:21:16 popularity:
[content:visits]
Case analysis of H series right-angle gearboxes in industrial wastewater treatment industry
This case study focuses on the renovation project of the core conveying and mixing system of a comprehensive industrial wastewater treatment plant in a large chemical industrial park. The project adopts customized corrosion-resistant H-series right-angle gearboxes to drive vertical sewage lift pumps and pool mixing equipment. It addresses core pain points such as limited space, rapid component corrosion, and axial impact overload in traditional direct-drive systems under high corrosion and high impurity wastewater conditions, achieving long-term continuous and stable operation of the wastewater treatment system.
🏭 Project background and original pain points
The wastewater treatment plant in this chemical industrial park is designed to treat 150,000 tons of industrial wastewater daily. The influent water contains high-concentration acids and alkalis, corrosive media, and a large amount of suspended solid impurities. The original system used conventional motors directly driving sewage pumps and mixing equipment, which revealed several serious issues during operation:
Severe spatial layout deficiency: The vertical space above the wastewater tank is only 2.7m, and the vertical motor is directly stacked above the pump body and mixing shaft. The total axial height of the unit exceeds 3m, resulting in insufficient lifting space for daily operation and maintenance. During disassembly and maintenance, it is necessary to temporarily remove the aeration and pipeline facilities on the top of the tank. Each maintenance session takes more than 36 hours, forcing the wastewater treatment system to operate at reduced capacity.
High corrosion failure rate: The surrounding area of the wastewater tank is permeated with high-humidity corrosive steam for a long time. The transmission components made of ordinary carbon steel material experience pitting corrosion on the shell and corrosion leakage at the shaft end seal after just 12 months of operation. On average, the seals need to be dismantled and replaced every four months, resulting in high operation and maintenance costs.
Axial impact overload occurs frequently: The large amount of suspended impurities and sludge clumps in the sewage can cause severe fluctuations in the load on the pump and mixing shaft, with axial thrust fluctuations reaching up to 50%. The original vertical motor comes with a thrust bearing with a rated load capacity of only 60,000N. Under the long-term influence of alternating impact loads, bearing burnout failures occur on average every 8 months, directly leading to the interruption of wastewater conveyance and thus preventing the timely treatment of industrial wastewater in the park. This poses a significant risk of environmental protection non-compliance emissions.
High energy consumption: The original direct-coupled drive scheme cannot flexibly adjust the rotational speeds of the pump and the agitator shaft. Instead, flow is regulated through valve throttling, resulting in significant energy loss. The annual power consumption of a single sewage pump exceeds 3.8 million kWh, and the overall energy consumption of the system far exceeds the industry average.
🛠️ Customized selection scheme for H series right-angle gearbox
For the special corrosion and heavy-load impact conditions of industrial wastewater treatment, the fully anti-corrosion upgraded H series right-angle gearbox is selected, with core configurations fully adapting to the stringent requirements of wastewater treatment scenarios:
Accurate matching of core parameters:
The horizontal motor is adapted with an input power of 750HP (approximately 560kW), with a 25% power redundancy reserved. Its rated input speed is 1500rpm, and through a customized transmission ratio of 1.4:1, the pump output speed reaches 2100rpm, fully matching the operating point of the sewage lift pump with a rated flow of 2000m³/h and a lift of 60m. At the same time, the speed of the mixing equipment can be flexibly adjusted to meet the mixing requirements of different wastewater pools.
The upgraded heavy-duty thrust roller bearing boasts a rated axial thrust capacity of 125,000N, fully covering the maximum instantaneous axial thrust of 92,000N on the pump and mixing shaft under the impact of impurities. With a 36% thrust redundancy reserved, it thoroughly addresses the bearing overload issues caused by alternating axial impact loads.
Special optimization for corrosion prevention in wastewater scenarios:
The gearbox housing is constructed with high-strength cast iron and coated with heavy-duty epoxy resin for corrosion protection. All exposed fasteners are made of 316L stainless steel, ensuring an anti-acid and alkali corrosion lifespan of over 8 years, significantly longer than the 1.5-year corrosion resistance of ordinary carbon steel. The gears are crafted from 20CrMnTi alloy steel, which undergoes carburizing and quenching treatments, and the surface is treated with anti-corrosion passivation to prevent corrosive steam from infiltrating and causing rust and wear on the tooth surface.
The shaft end adopts a dual double-lip seal consisting of fluororubber and PTFE, elevating the protection level to IP55. It fully resists the intrusion of high-humidity corrosive steam and wastewater splashes into the interior, effectively preventing lubricant leakage and malfunctions caused by corrosion of internal components.
Layout and operation and maintenance adaptation optimization:
The horizontal motor is arranged horizontally in a safe area on the ground next to the wastewater tank. After a 90° turn through the H series right-angle gearbox, it vertically outputs to drive the vertical sewage pump and mixing shaft. The total axial height of the unit is reduced from 3m to 1.6m, perfectly fitting the narrow vertical space above the wastewater tank. There is no need to modify the original steel structure on the top of the tank, significantly reducing the cost of renovation and construction.
Equipped with online monitoring sensors for oil level and temperature, they are integrated into the DCS control system of the wastewater plant, enabling real-time remote monitoring of the gearbox's operating status. This allows for early prediction of potential failures, thus preventing sudden failures during unattended periods.
✅ Actual test results of project implementation
After being put into operation, the renovation project has been continuously running for 30 months without any major malfunctions, and its various performance indicators far exceed the industry standard requirements:
Reliability significantly improved: The gearbox's heavy-duty thrust bearing fully bears all the alternating axial loads of the pump and mixing shaft, with the shaft vibration value stabilized below 2.8mm/s, completely eliminating the original motor thrust bearing burnout failure. The continuous trouble-free operation time of the equipment has been extended from 8 months to 30 months, and the reliability of the wastewater treatment system has been improved to 99.9%, completely avoiding the risk of environmental protection emission exceeding standards.
Significant Energy-Saving Benefits: Through precise matching of gearbox transmission ratios and eliminating the original valve throttling adjustment, the system transmission efficiency has been increased to 97%. Each sewage pump saves 2.6 million kWh of electricity annually. Calculated at an industrial electricity price of 0.65 yuan/kWh, the annual direct additional income exceeds 1.69 million yuan, and the total transformation cost can be recovered in just 12 months.
Significant enhancement in corrosion resistance: The equipment has been continuously operating for 2.5 years in a high-humidity corrosive steam environment, with no visible pitting on the shell and no oil leakage from the shaft end seal. The replacement cycle of seals has been extended from 4 months to 24 months, resulting in a 75% reduction in annual operation and maintenance costs.
Operational and maintenance efficiency has been significantly improved: After the overall height of the unit was significantly reduced, routine maintenance can be directly completed using on-site conventional cranes for lifting. The time for single pump disassembly and maintenance has been shortened from 36 hours to 6 hours, and the downtime for maintenance of the wastewater treatment system has been reduced by 80%, significantly reducing the environmental risks during system downtime.
📌 Summary of core project experience
When selecting models for industrial wastewater treatment scenarios, priority must be given to anti-corrosion upgrades. The shell, fasteners, and seals should all be made of acid and alkali-resistant materials. It is prohibited to directly use ordinary land standard models, as they will experience severe corrosion failure within 1 to 2 years.
The alternating axial impact caused by suspended impurities and sludge clumps is a core pain point in wastewater treatment systems. It is necessary to select customized H series models with high thrust capacity, reserving more than 30% of axial thrust redundancy to avoid early fatigue damage to bearings caused by alternating loads.
This solution can be directly replicated and promoted to various wastewater treatment scenarios with high corrosion and heavy load impact, such as chemical industrial park wastewater treatment, municipal sewage plants, and printing and dyeing wastewater treatment. It is the mainstream technical route for current wastewater treatment systems to reduce costs, increase efficiency, and enhance operational reliability.
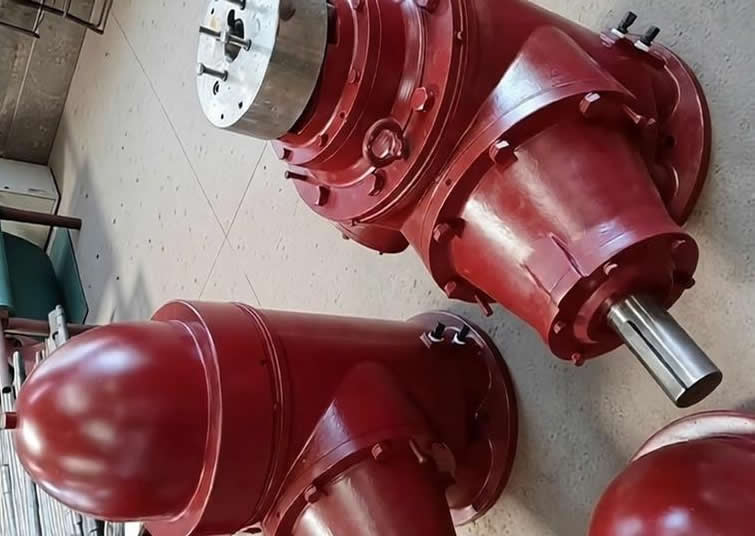
Project Background: A state-owned wastewater treatment plant in Changsha has customized two vertical long-shaft pumps with a submerged depth of 14 meters, equipped with H series right-angle gearboxes, for industrial wastewater/wastewater treatment.
Technical points:
· Submerged depth: 14 meters
· Pump type: vertical long-shaft submerged pump (LC series)
· Application: Industrial wastewater treatment
Analysis: A submergence of 14 meters indicates an extremely long pump shaft, necessitating the installation of an intermediate bearing in the middle of the pump body in traditional solutions. After adopting the right-angle gearbox solution:
The drive end is positioned above the liquid level, facilitating maintenance
· The gearbox bears all the axial loads of the upper pump shaft
· Reduced structural complexity and failure rate of the submerged part
label: Series,H,Gearboxes,Right-angle,Gearbox

 HOTLINE:+8613974960765 +8618507312158


 Service Hotline +8613974960765
